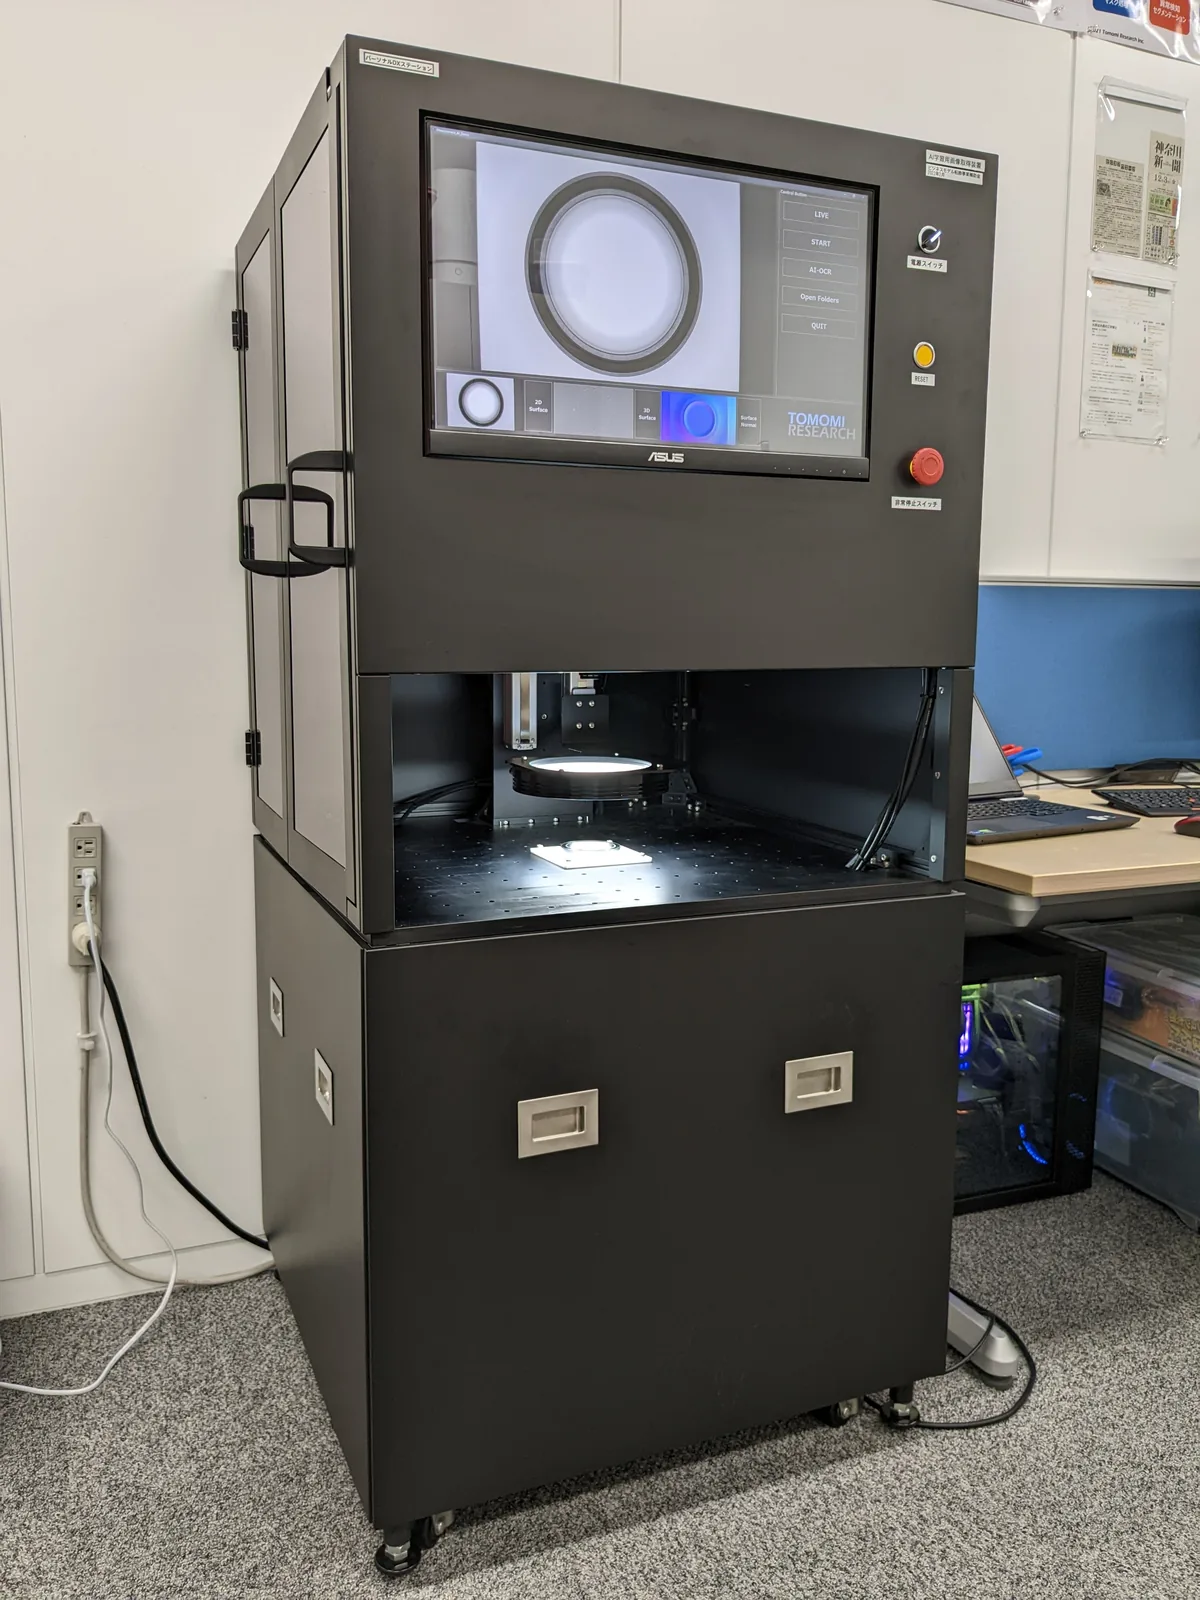
TR-100 / AI visual inspection system
Make it visible,
then decide on it.
TR-100 images the surface with FORESIGHT STEREO and returns a verdict with E3 ENGINE. From a unit that sits on a bench to an in-line configuration wired to a PLC, robot and conveyor, the way of seeing stays the same and only the scale changes.
What it shows
Take the colour away,
and the shape stands up.
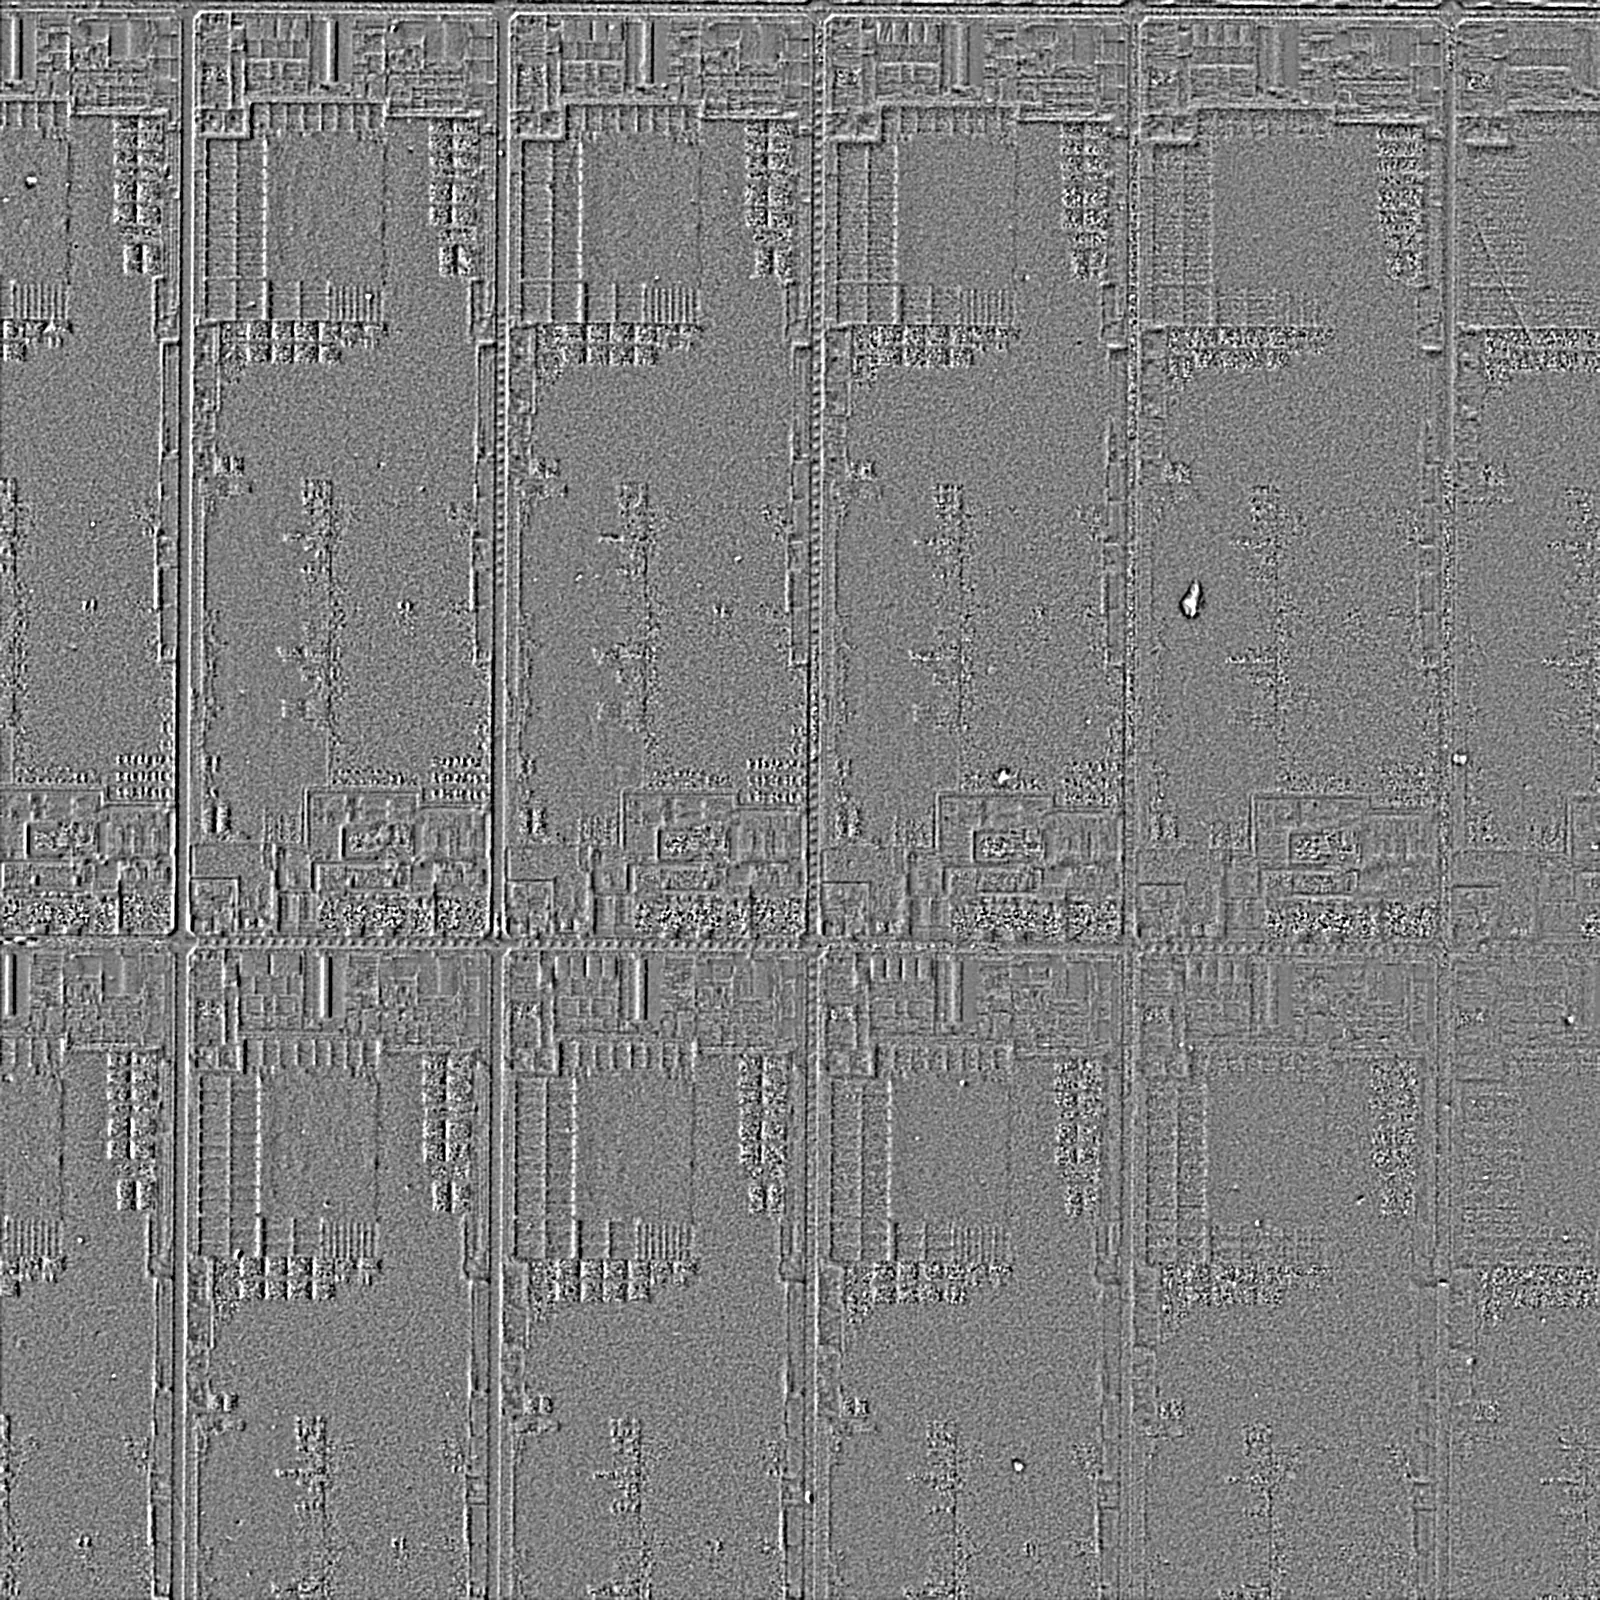
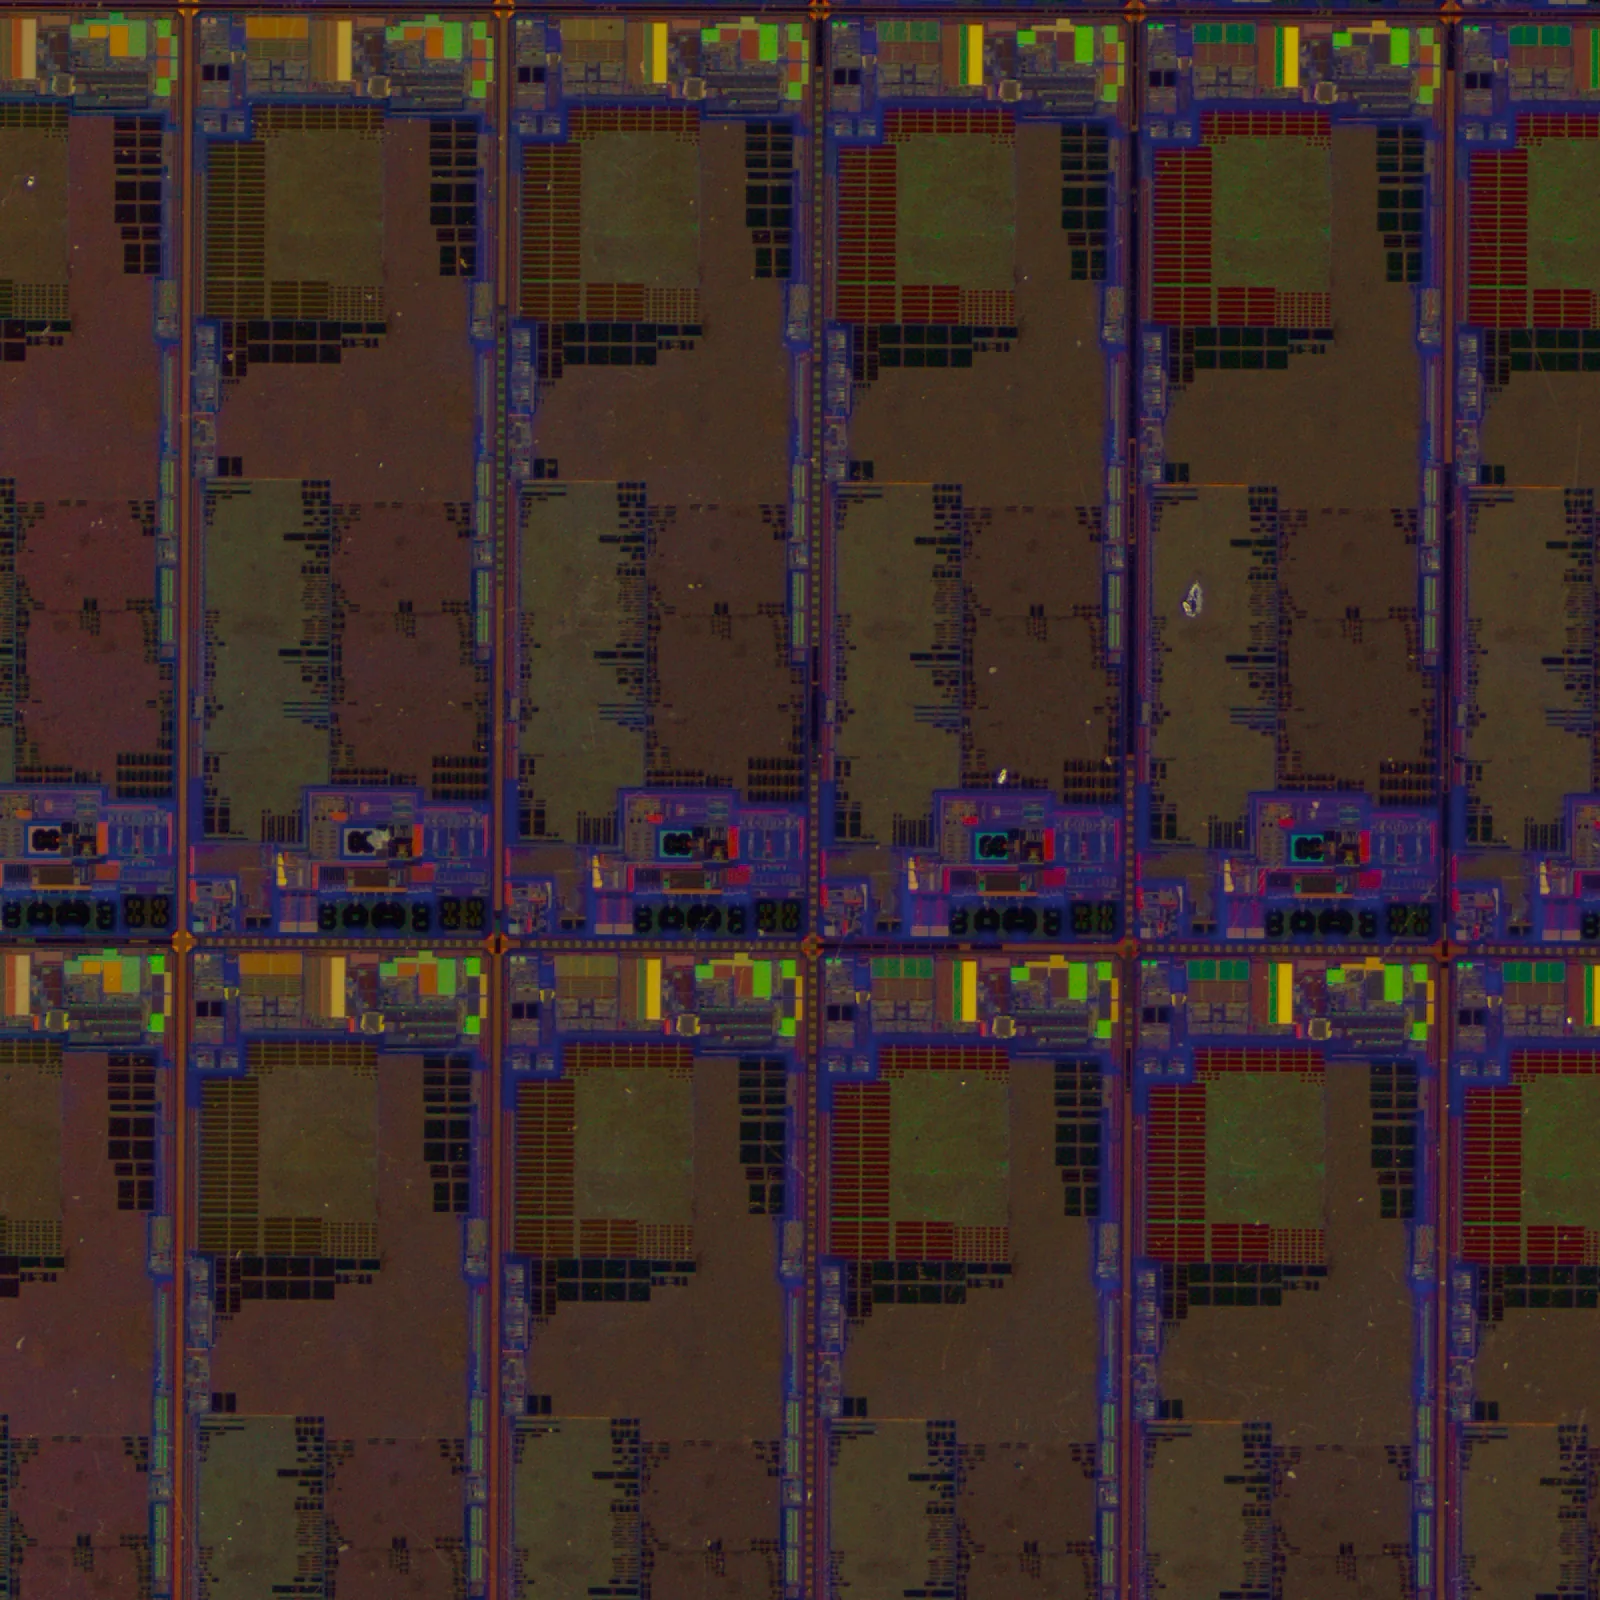
The surface of a semiconductor chip is a mixture of purple, green, red and blue — interference colours produced by thin films. The shape that matters is lost in that brilliance. From one and the same capture, TR-100 separates the image that is only colour from the image that is only shape.
◀ Drag to compare ▶
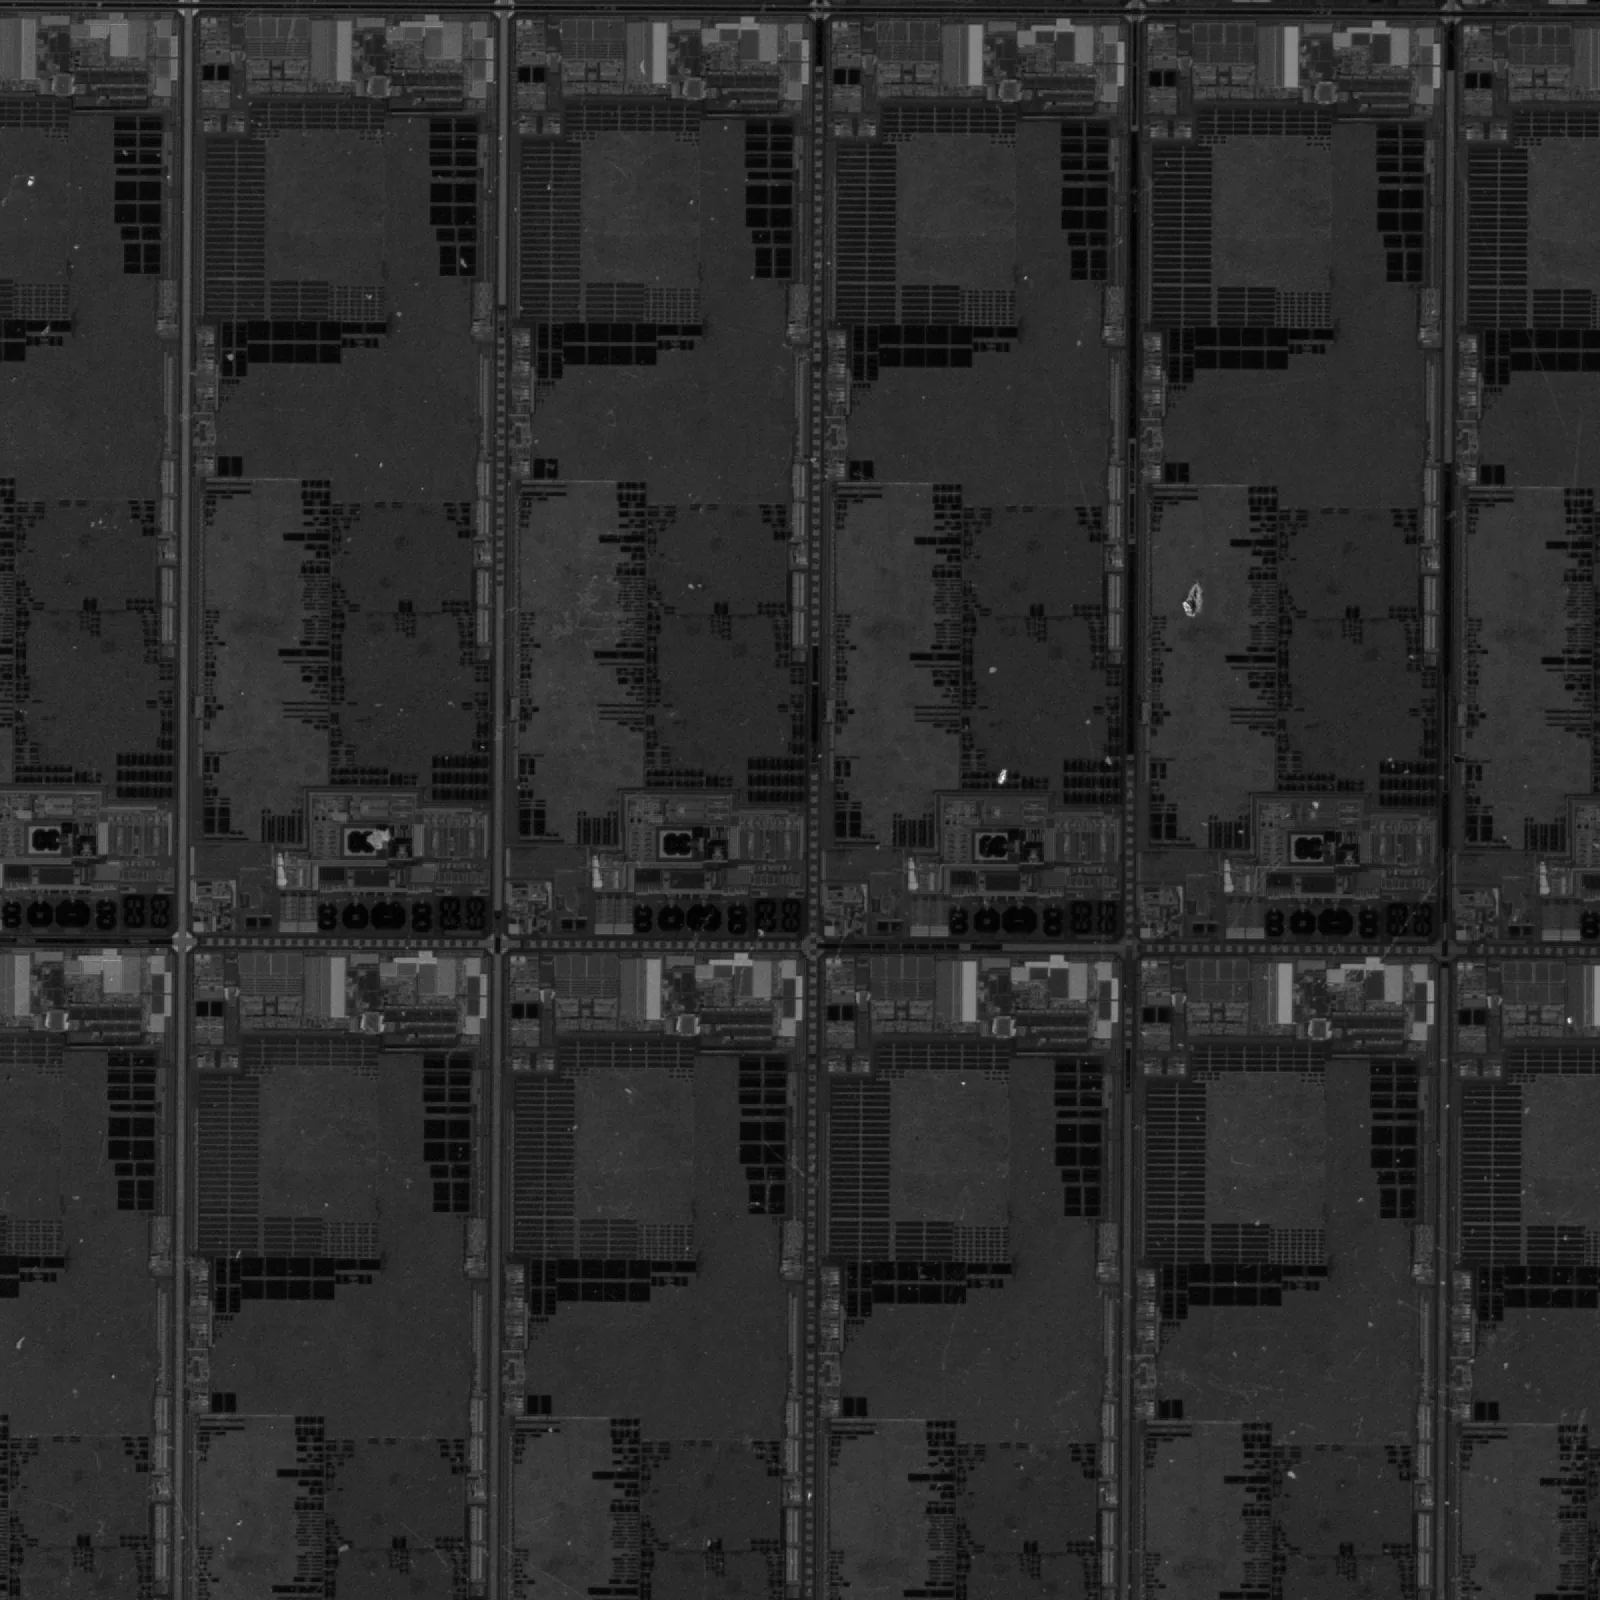
A grid of dies and the scribe-line grooves that divide them. Most of the colour that was vivid in the live image does not appear in the 3D Surface; what remains is the relief that the colour had been hiding.
※ This is a demonstration on one sample, and does not guarantee general detection or measurement performance. All four outputs of the same subject are published on our technical blog (2026-06-16).
Four outputs
One capture. Four outputs.
These are not four separate captures. They are four ways of reading one and the same capture. Which one is used for the decision is chosen to suit what you need to see.
The image as the eye sees it.
The ordinary capture, kept as the reference. Interference colours and reflections remain. The starting point.
Shading discarded, material kept.
The lighting is taken out and the albedo extracted. What pattern sits where reads plainly.
Material discarded, shape kept.
Interference colours vanish; the steps of the wiring and the scribe-line grooves remain as relief. What was colour and not shape becomes clear.
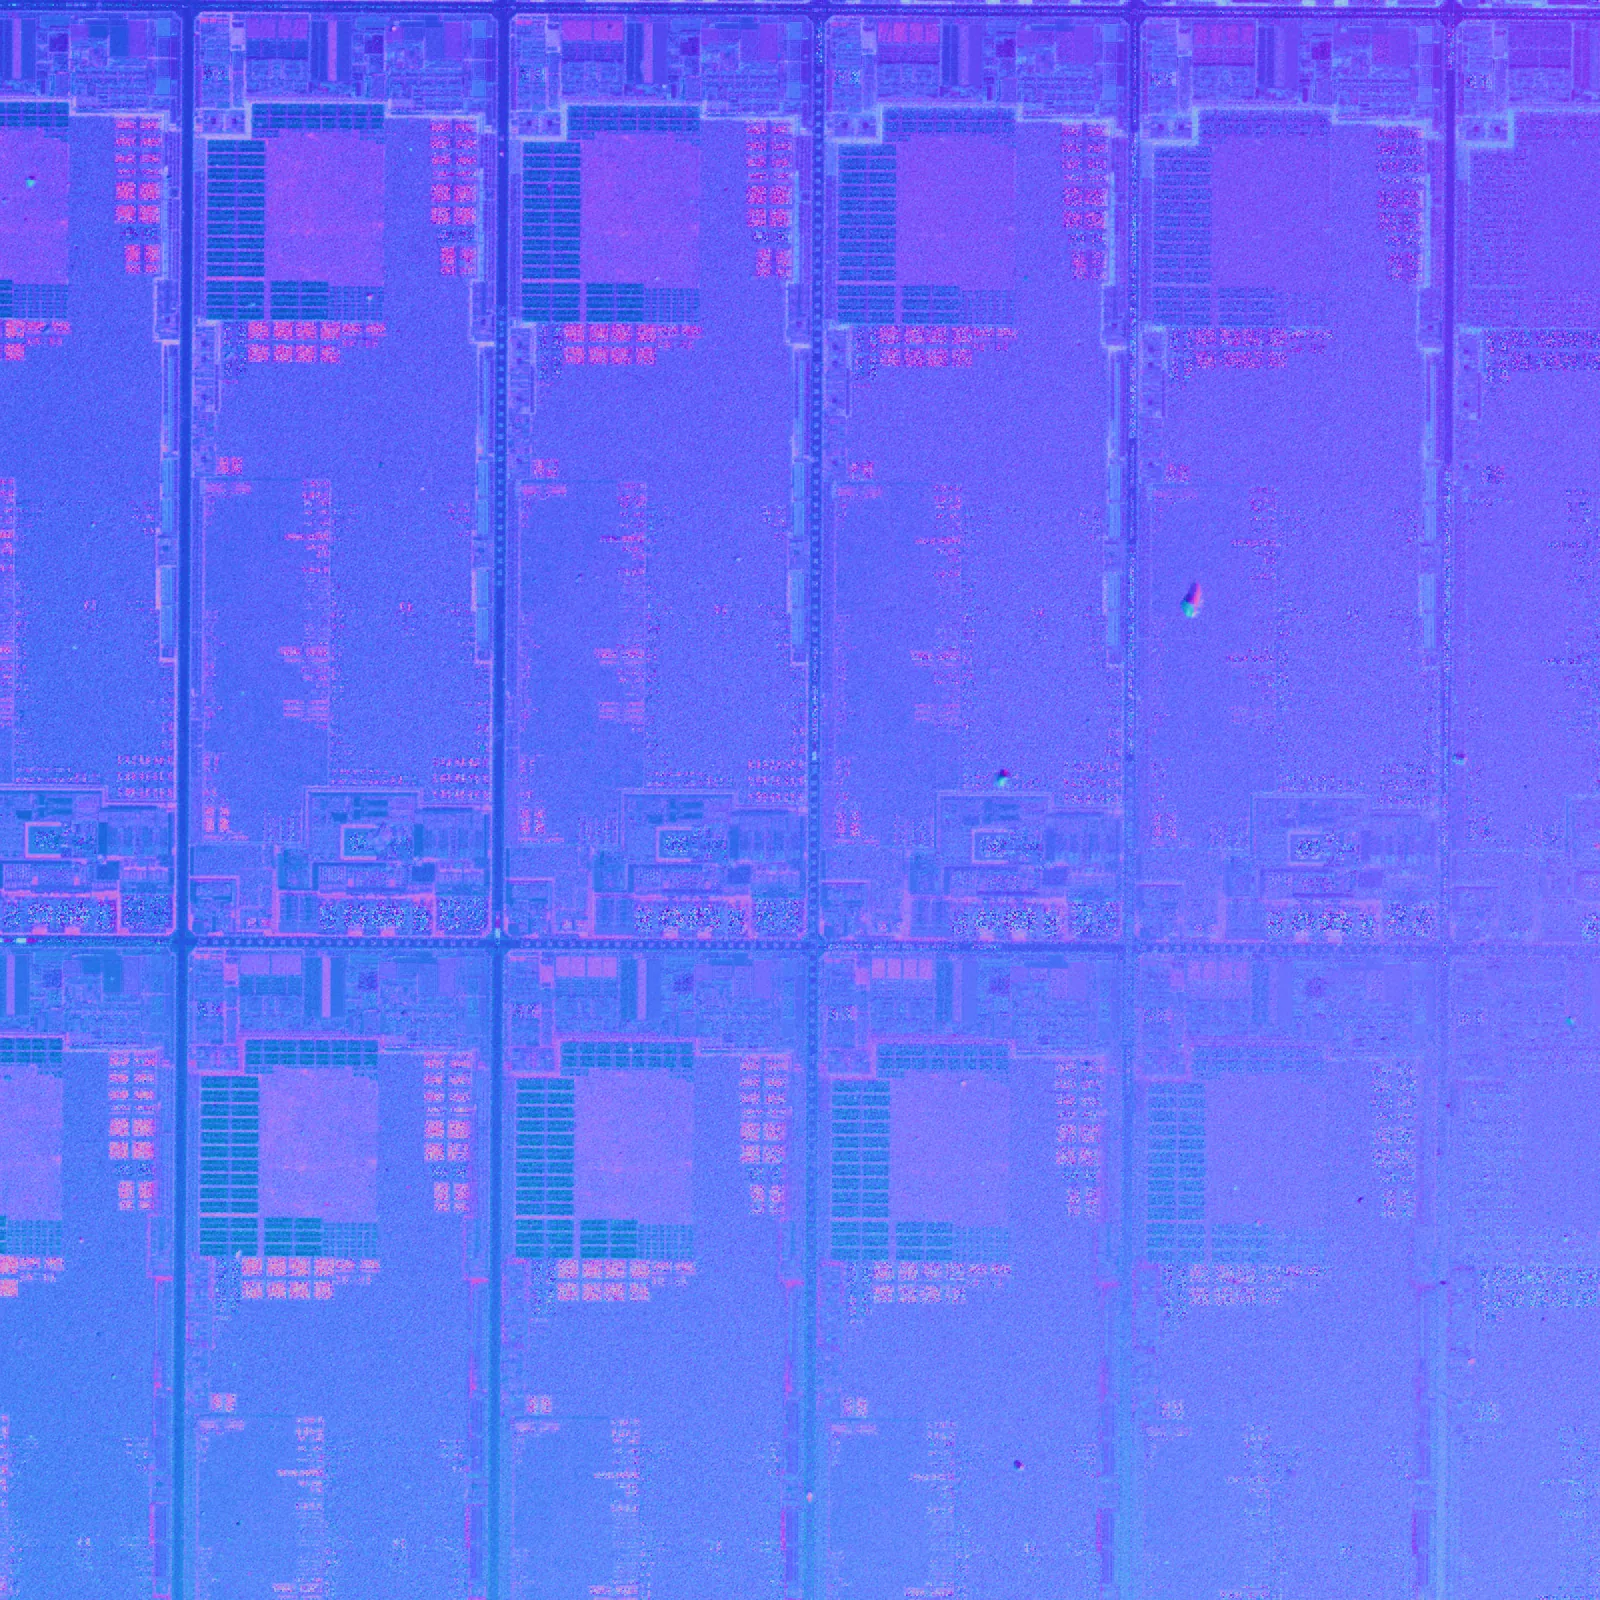
Surface direction, encoded as colour.
A feature independent of the lighting. Most of the face points straight up and reads as a single colour, so only the edges stand.
From seeing to deciding
Seeing is not
where it stops.
After the capture, TR-100 returns a verdict through the E3 ENGINE it carries. That is what separates it from a unit built for observation.
◀ Drag to compare ▶
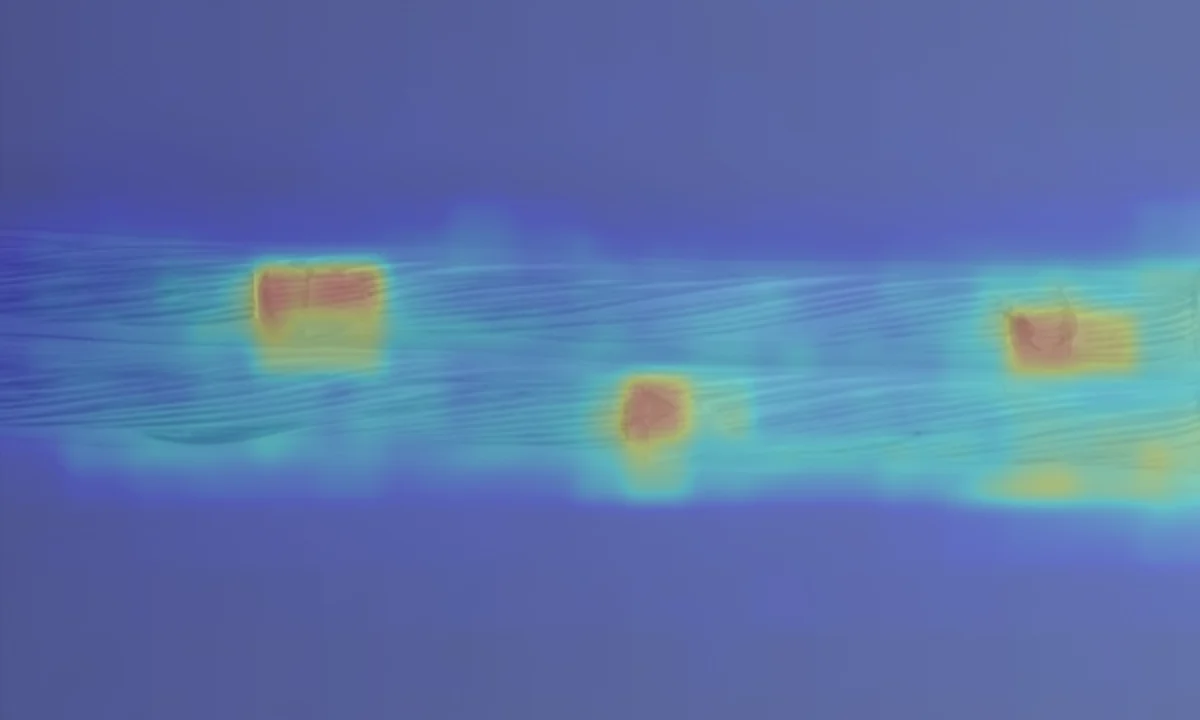
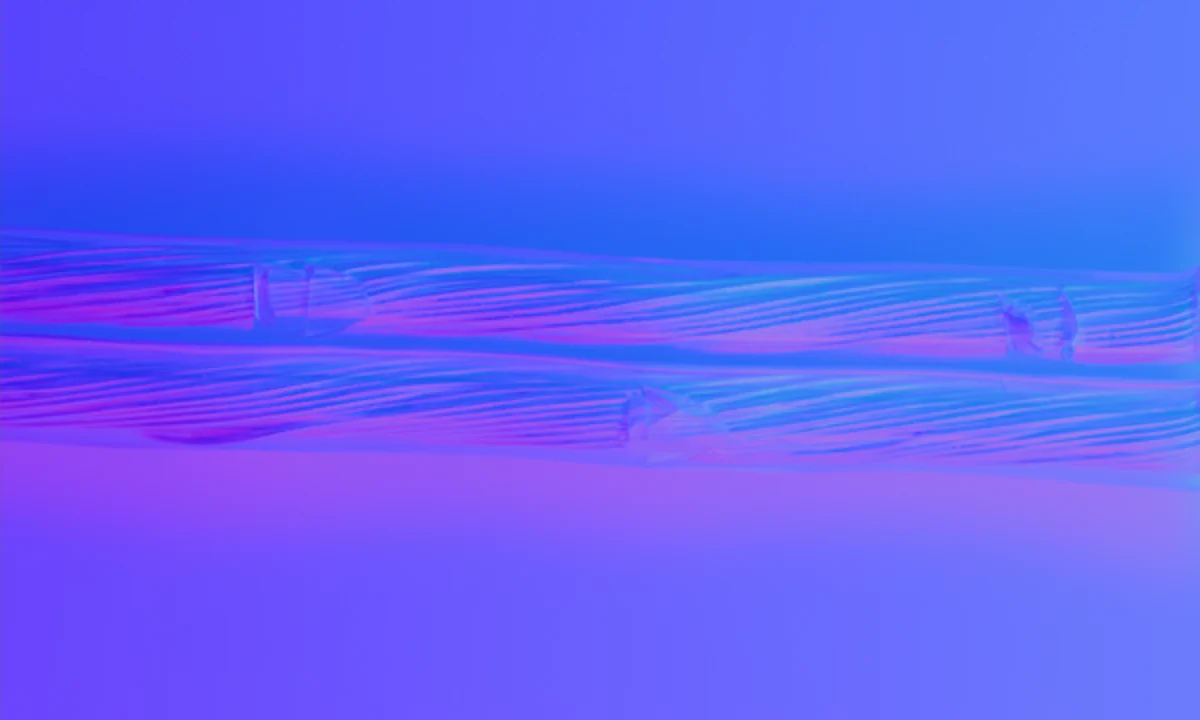
Enamelled wire for an electric motor. Damage to the transparent insulating coating barely shows as colour, but it does show as a disturbance in surface direction. E3 ENGINE points at those three places, and does not react to the sound stretches.
It learns from good products only
It does not assume a process of collecting defects and labelling them. It puts a number on the something not present in a good one. In the example above, only good pieces were used for training.
The verdict is three-way
OK / Human_Check / NG. The band the machine cannot settle is returned to a person.
You choose which output it decides on
Decide on the Live image, or decide on the Surface Normal. Before the algorithm, you can change what is looked at.
The same flaw, a different result,
depending on what you hand over.
Point 03 above can be checked by measurement rather than argued in words. These are the score maps for the same enamelled wire, trained and evaluated on the Live image, as a person sees it, and on the Surface Normal from FORESIGHT STEREO.
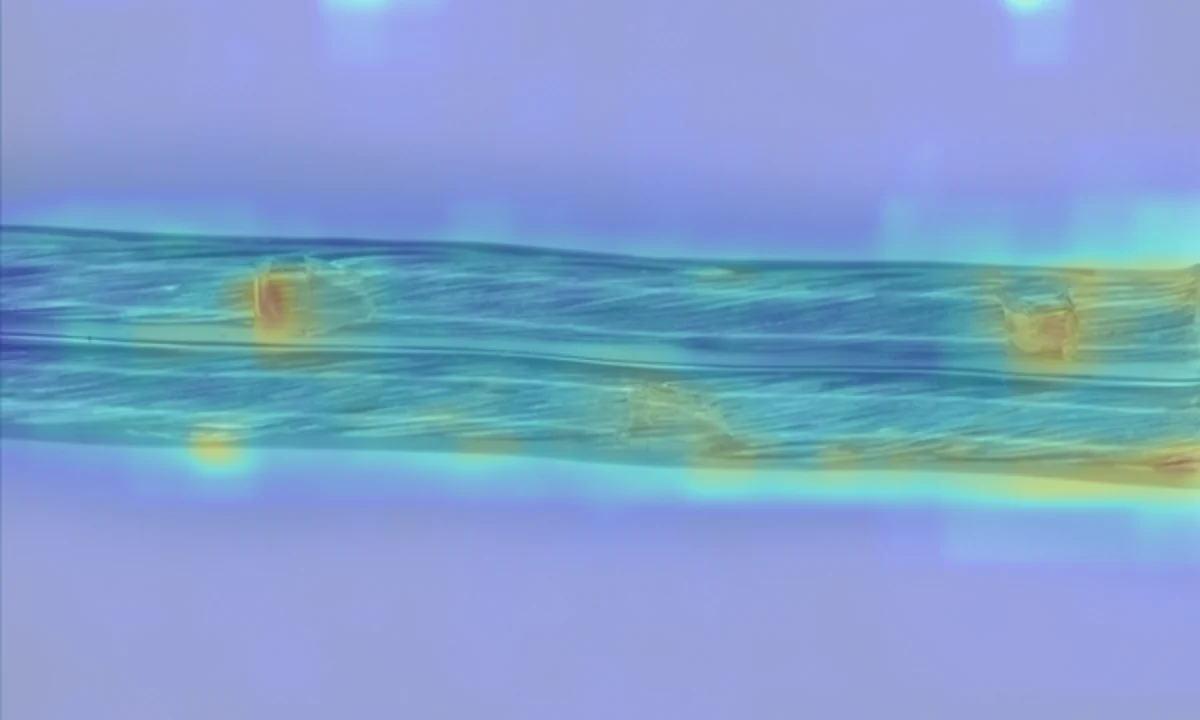
The response spreads beyond the flaw.
It does react to the flaws. But warm colour also lands on sound strands and on the edges, so where to look cannot be narrowed down.
The response stands only on the flaw.
Hand over surface direction, which does not depend on the lighting, and the flicker of gloss falls away. What remains is the anomaly of shape.
※ Conditions for the two maps above ─ Surface Normal: trained on 63 good pieces; evaluated on 14 good and 7 defective. Live: trained on 61 good pieces; evaluated on 10 good and 7 defective. Because the counts for training and evaluation do not match, this is not a strict comparison in which only the input was swapped. It is what was observed on this one specimen, and does not guarantee that the same difference appears for every object 〔同一条件での再評価: 要確認〕.
※ Training needs good pieces only, but calibrating the threshold needs real examples of defects. E3 ENGINE returns a verdict; it does not classify the type of defect. More on E3 ENGINE →
Three configurations
From the bench,
into the line.
The way of seeing does not change; only the way it is installed does. From checking samples one at a time through to running automatically inside a process, the thinking stays the same.
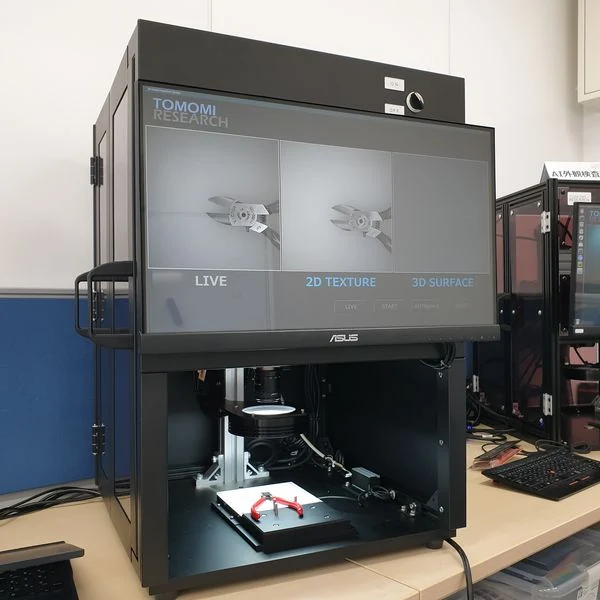
For small-scale inspection, and for research.
A configuration for smaller companies and for researchers. Set a sample down, capture it, and check the result on the spot.
For building into a process.
A configuration for medium-scale manufacturers and production engineers. It carries an interface IO board linking the PLC and the PC.
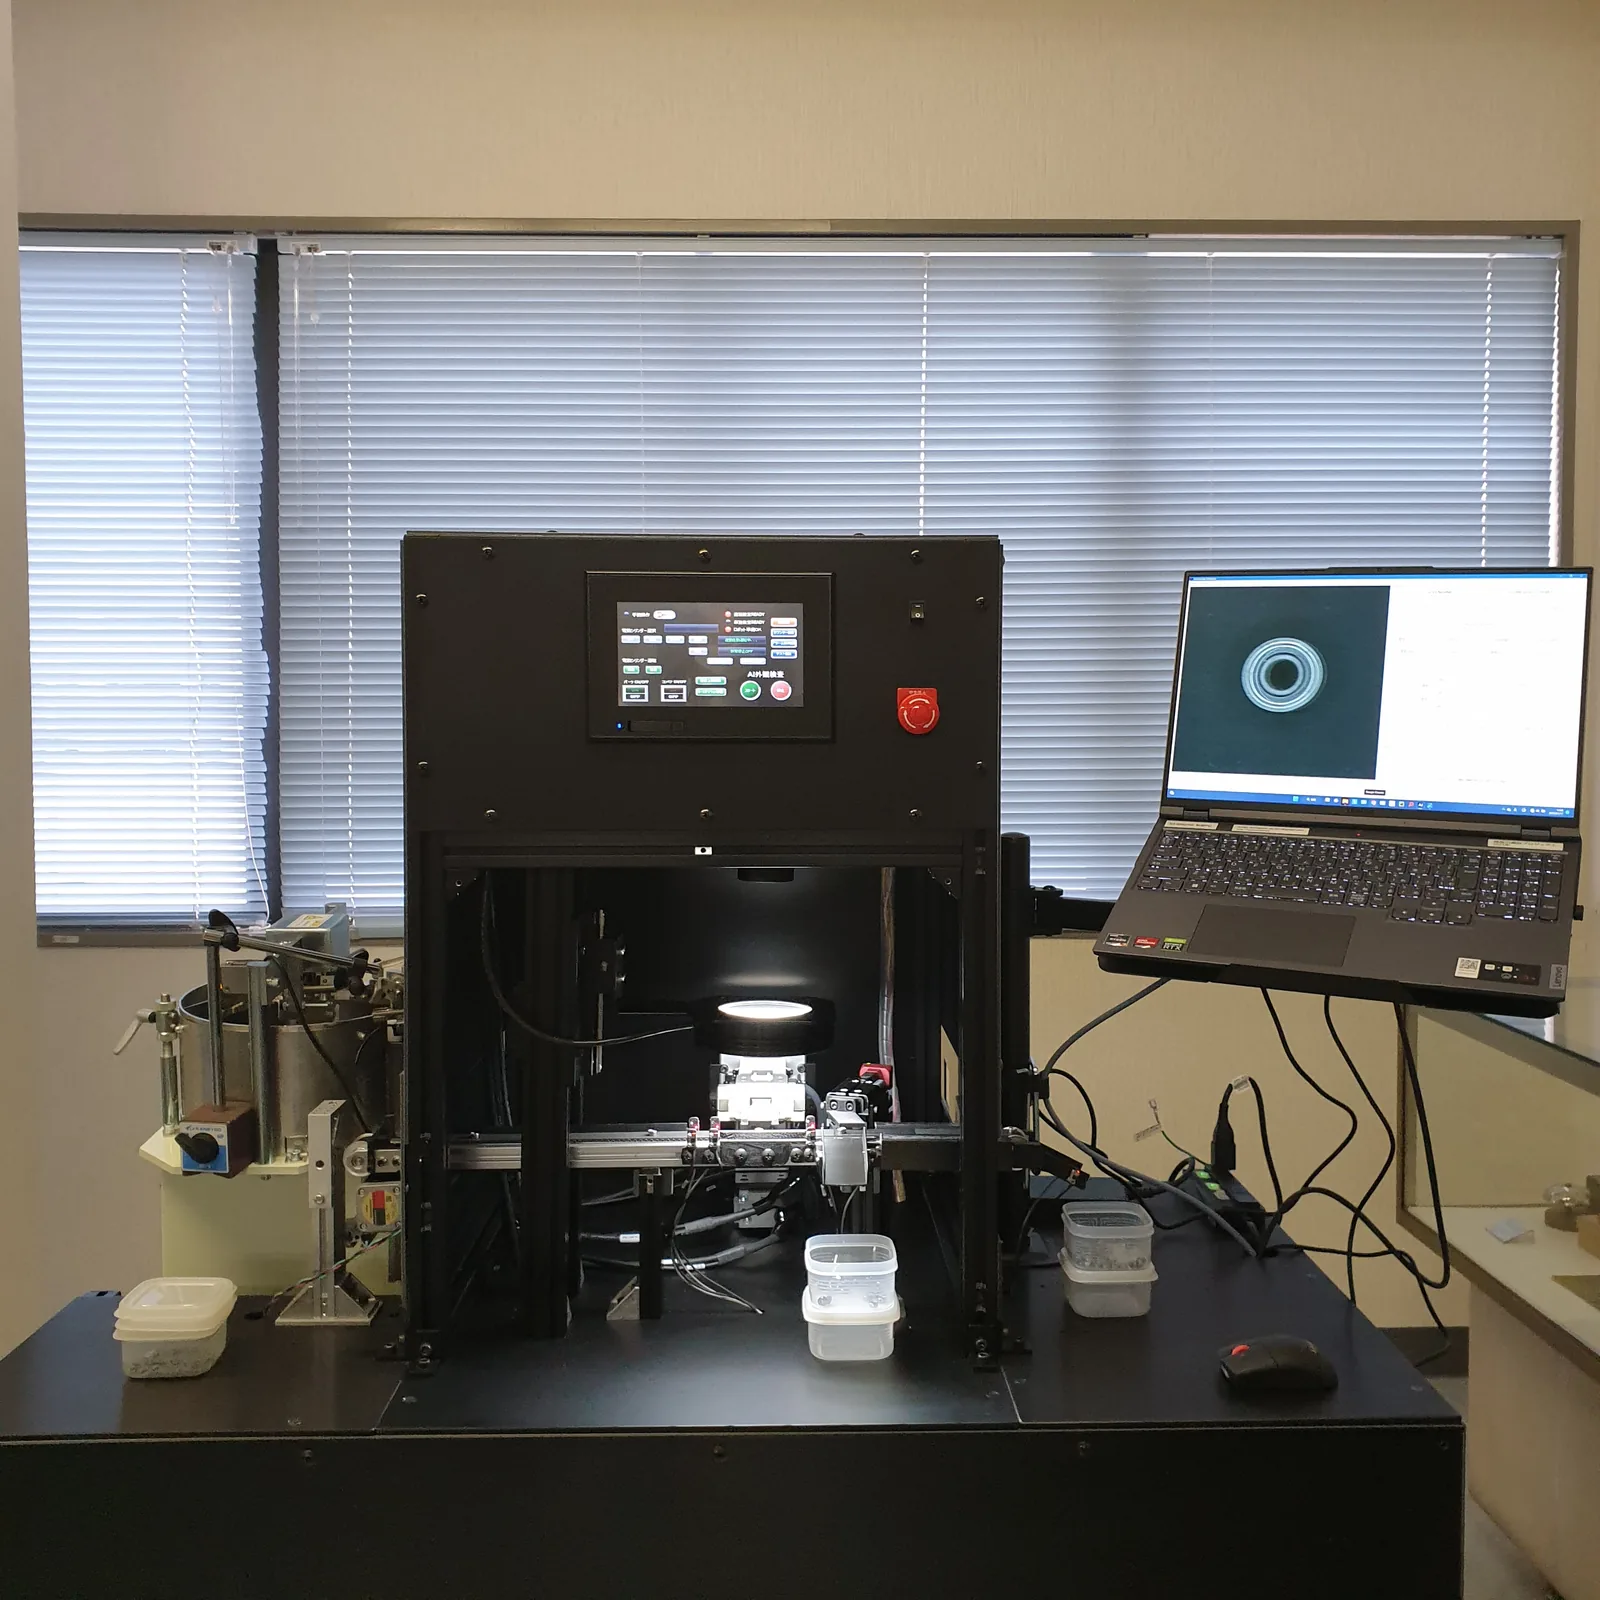
For running a line automatically.
The in-line type, suited to automated inspection systems in a factory. The configuration includes the PLC, the interface IO board, a robot and a belt conveyor.
〔要確認〕 The names of the configurations follow the current product page (Desktop / Standard / Premier). The 2022 catalogue writes them as BASIC / STANDARD / PRIMERE and lists camera pixel counts and functions per configuration. The naming and the correspondence need to be settled.
What it has looked at
What it has been asked to see.
In every case the difference is hard to catch in colour or brightness and appears only as a difference in shape. The following are the application examples given in our published catalogue.
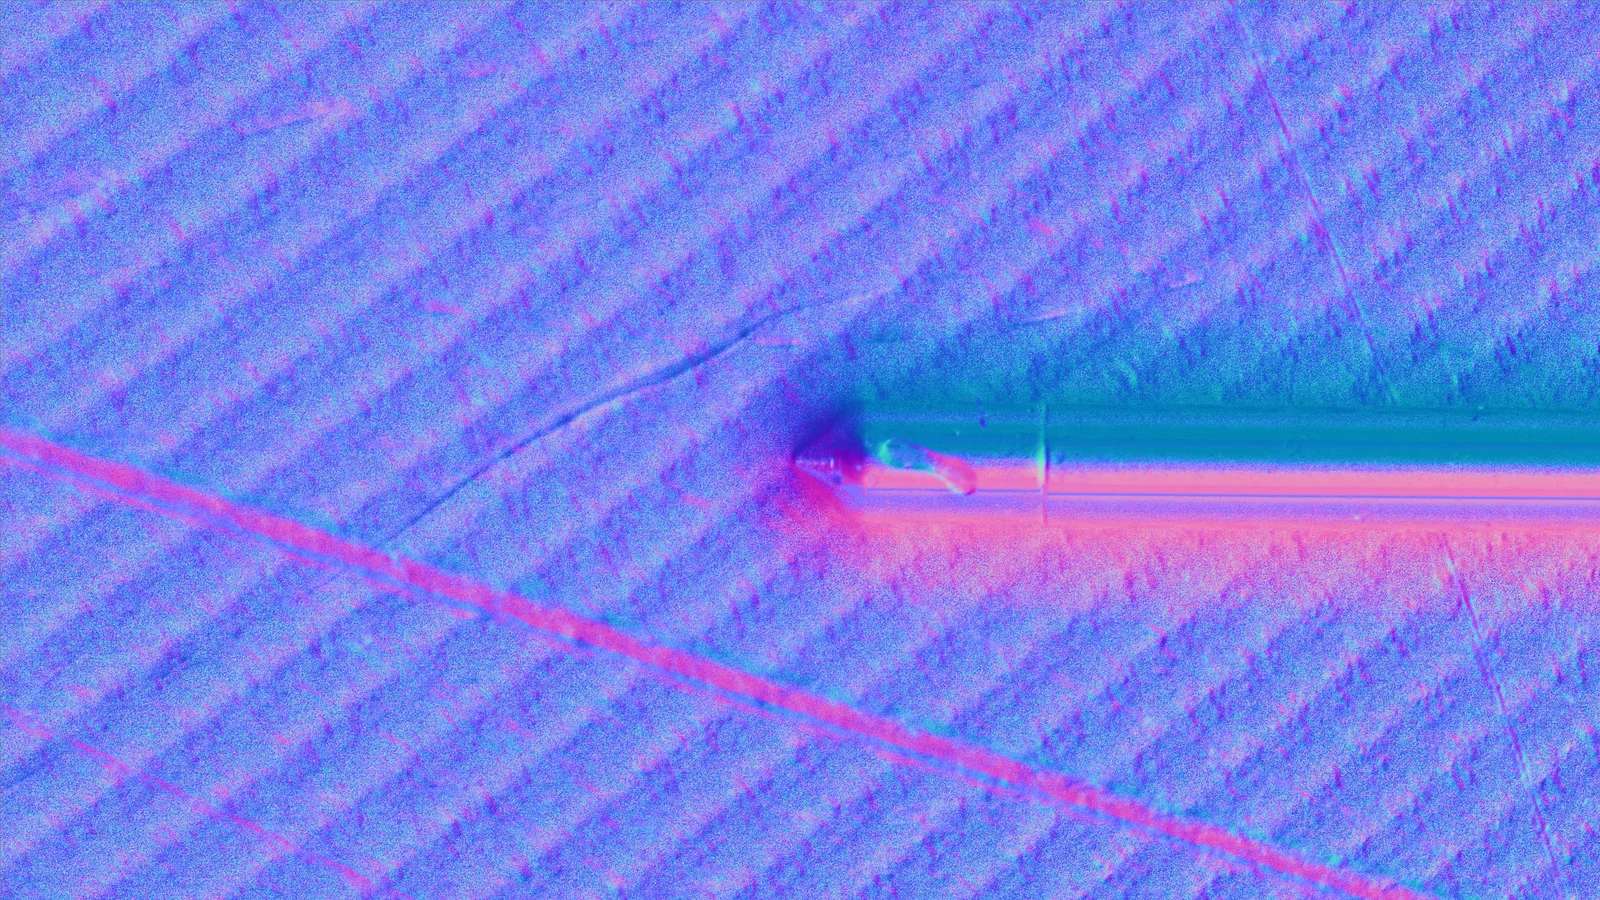
◀ Drag to compare ▶
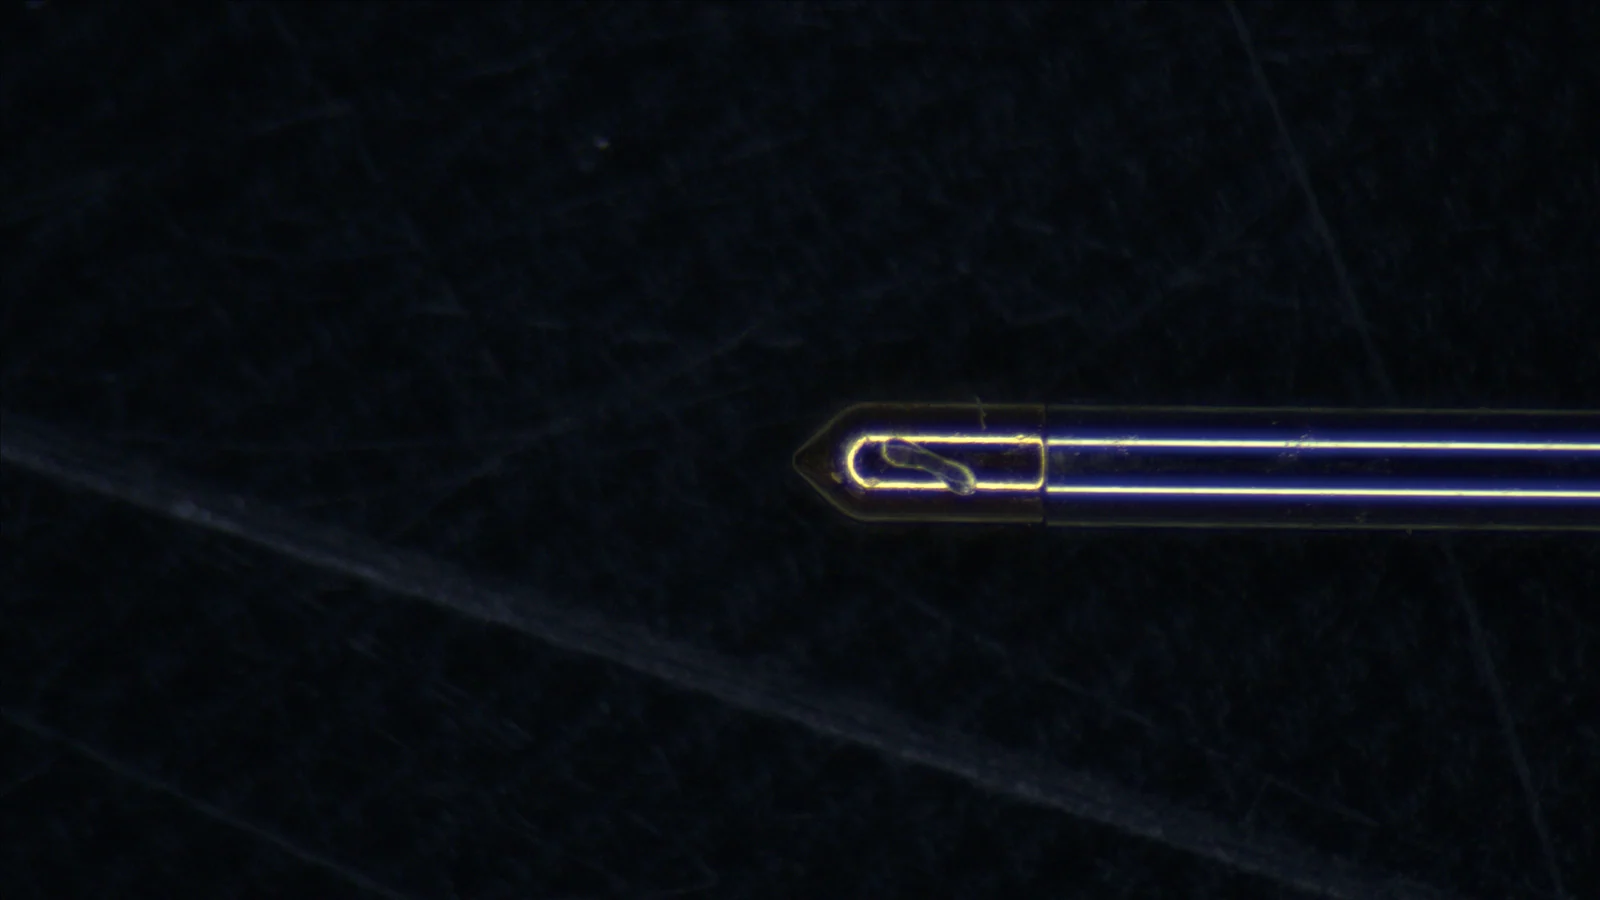
The machined face of a metal tool. In an ordinary capture it sinks almost to black and even the scratch the needle is pointing at cannot be read. In the surface normal, the machining striations and the scratch crossing them separate as a difference in direction.
Bearings
Height anomalies in the shield. Reflection from the gloss makes the hollows hard to confirm under conventional lighting.
Wire for electric motors
Flaws in the transparent insulating coating, which barely appear as a difference in colour. This is the subject of the example above →
Discolouration of metal surfaces
Surface anomalies on a 100-yen coin.
Metal tools
Scratches and dents on glossy surfaces.
〔要確認〕 These are the application examples given in the catalogue. Customer names, installation records and figures for savings are not published here until permission and accuracy have been confirmed.
Specifications
What has been published.
TR-100 is a product whose optics are designed around the object. Camera, lens and field of view are selected according to the object and the size to be detected.
| Category | AI visual inspection system |
|---|---|
| Configurations | TR-100 Desktop / TR-100 Standard / TR-100 Premier (see Three configurations) |
| Imaging | FORESIGHT STEREO® (a 3D imaging technique developed from photometric stereo) |
| Outputs | Live / 2D Texture / 3D Surface / Surface Normal (all four from a single capture) |
| Decision | E3 ENGINE® (an anomaly detection engine that learns from good products only, returning OK / Human_Check / NG) |
| External interfaces | An interface IO board linking PLC and PC / connection to upper-level equipment (PLC, robot) over Modbus TCP / integration with robots and belt conveyors |
| Image storage | A NAS for image storage is included as standard |
| Functions by configuration | Imaging (FORESIGHT STEREO®) and AI decision (E3 ENGINE®) are common to all three configurations. |
| Camera | Standard is an 8.3 MP area-scan camera. Up to 24.4 MP can be specified. |
| Field of view and resolution | Field of view ranges from about 80 mm in diameter at the narrow end to 300 mm square. Camera, lens and working distance are selected according to the object and the size to be detected. Pixel resolution is the field width divided by the horizontal pixel count of the camera. We recommend that the resolution you need be settled by prior evaluation on your own samples. |
| Work | Metal, plastic, ceramic, semiconductors and electronic components. The targets are surfaces that ordinary imaging struggles with: glossy faces, low-contrast faces, fine relief. Work size depends on the configuration and the optics. |
| Dimensions | W 700 × D 700 × H 1500 mm (TR-100 Standard). Designed around work size and handling, so it varies by configuration. |
| Power and environment | Indoor use. Power: AC 100 V. PC and GPU are selected to suit the configuration. |
| Options | Different cameras and lenses, integration with robots and handling, OCR and dimensional measurement modules. Rule-based custom image processing is also supported. |
※ Whether something can be detected depends on the object, the kind of defect and the imaging conditions. The images on this page are the result of observing and analysing particular samples, and do not guarantee performance for every object or inspection condition. “Visible” here means physically based observation and visualisation, not generative estimation.
Where it sits
TR-100 in the three layers.
Our products are built in three layers. TR-100 sits in the systems layer, in a configuration that holds both the sensor and the decision in one unit.
FORESIGHT STEREO®
A 3D imaging technique developed from photometric stereo. From illumination in many directions it takes the surface normal, independently of the lighting, and recovers 3D shape. It is the imaging side of TR-100.
E3 ENGINE®
The anomaly detection engine. It learns from good products only and puts a number on the “something not present in a good one” that an inspector senses. It is the decision side of TR-100.
TR series
The systems that carry the sensor. The configuration is chosen to suit the conditions and the purpose. TR-100 covers imaging through to decision in one unit; TR-55 is for observation, and TR-300 for continuous inspection on a moving line.
Recognition
Judged from outside.
Kanagawa Nadeshiko Brand 2024
Organised by Kanagawa Prefecture. The certified product is named “AI visual inspection system TR-100”. It is a scheme the prefecture set up to support outstanding women entrepreneurs and companies where women play a leading part, and to make their work widely known. Our announcement was dated 2024-02-06.
Covered by Nikkan Kogyo Shimbun
An interview article about TR-100 was published (2022-10-18).
〔要確認〕 The article URL, and whether the certification logo and the printed page may be reproduced, need separate confirmation.
Related
Related products
The anomaly detection engine on the decision side of TR-100. It learns from good products only and returns OK / Human_Check / NG.
Read more →
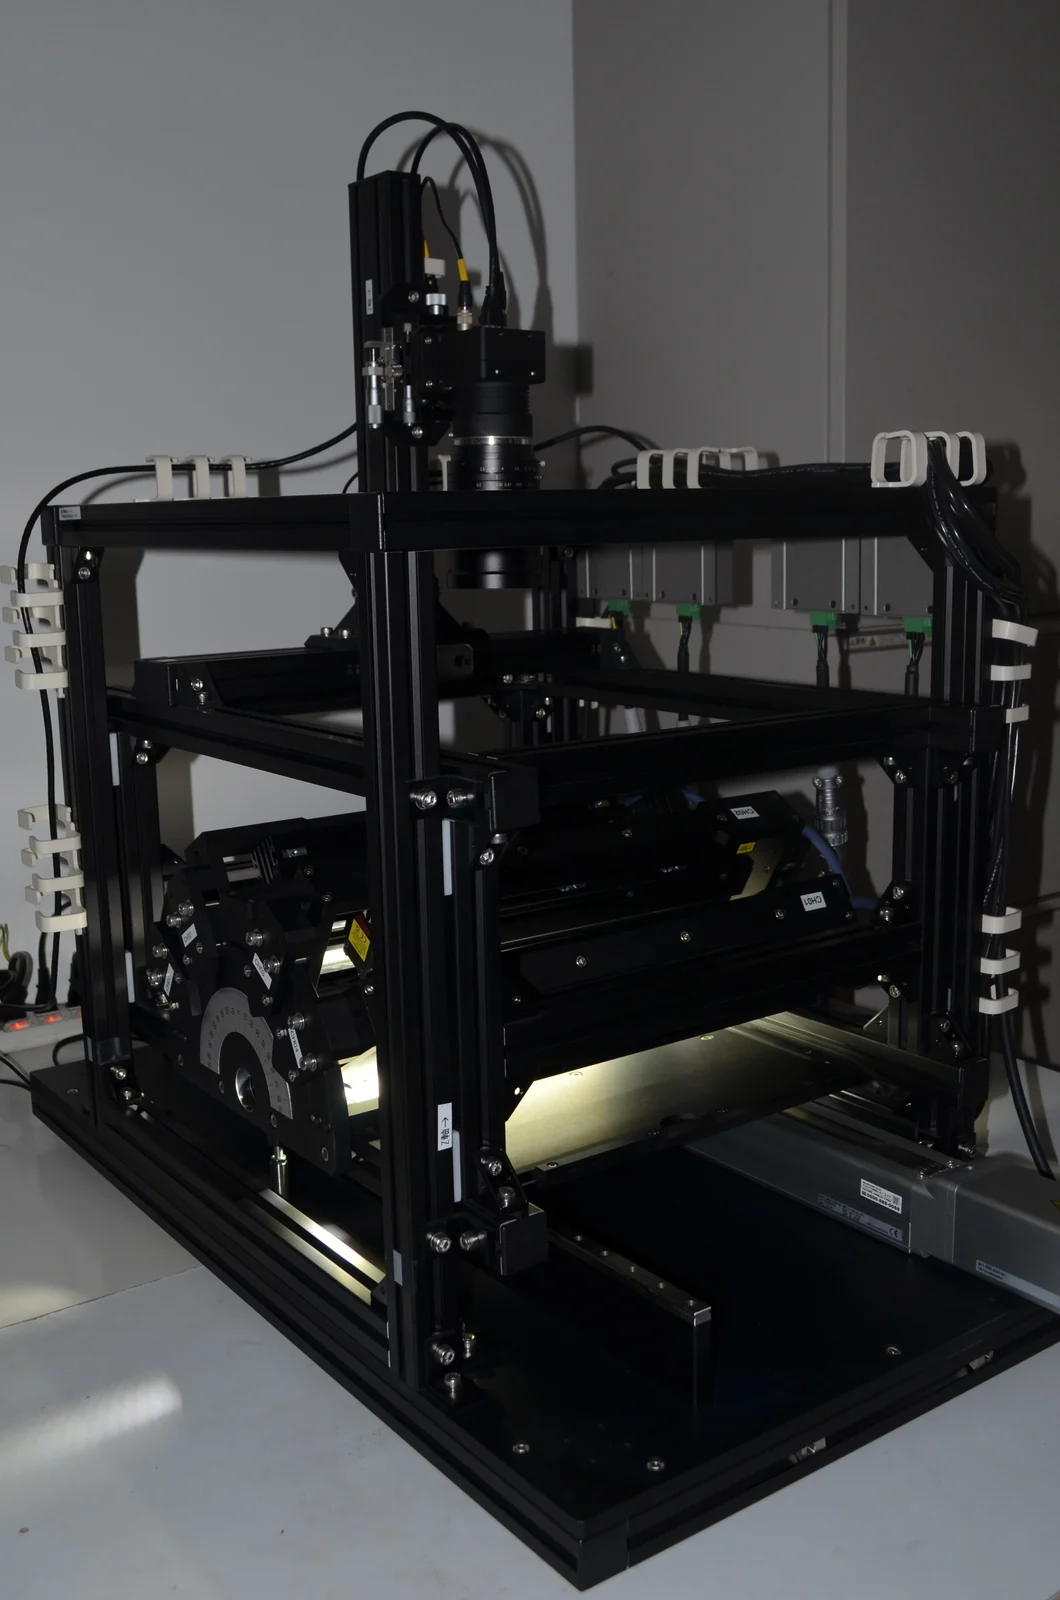
Seeing without stopping the line. Continuous inspection that forms a 3D image while the work moves.
Read more →
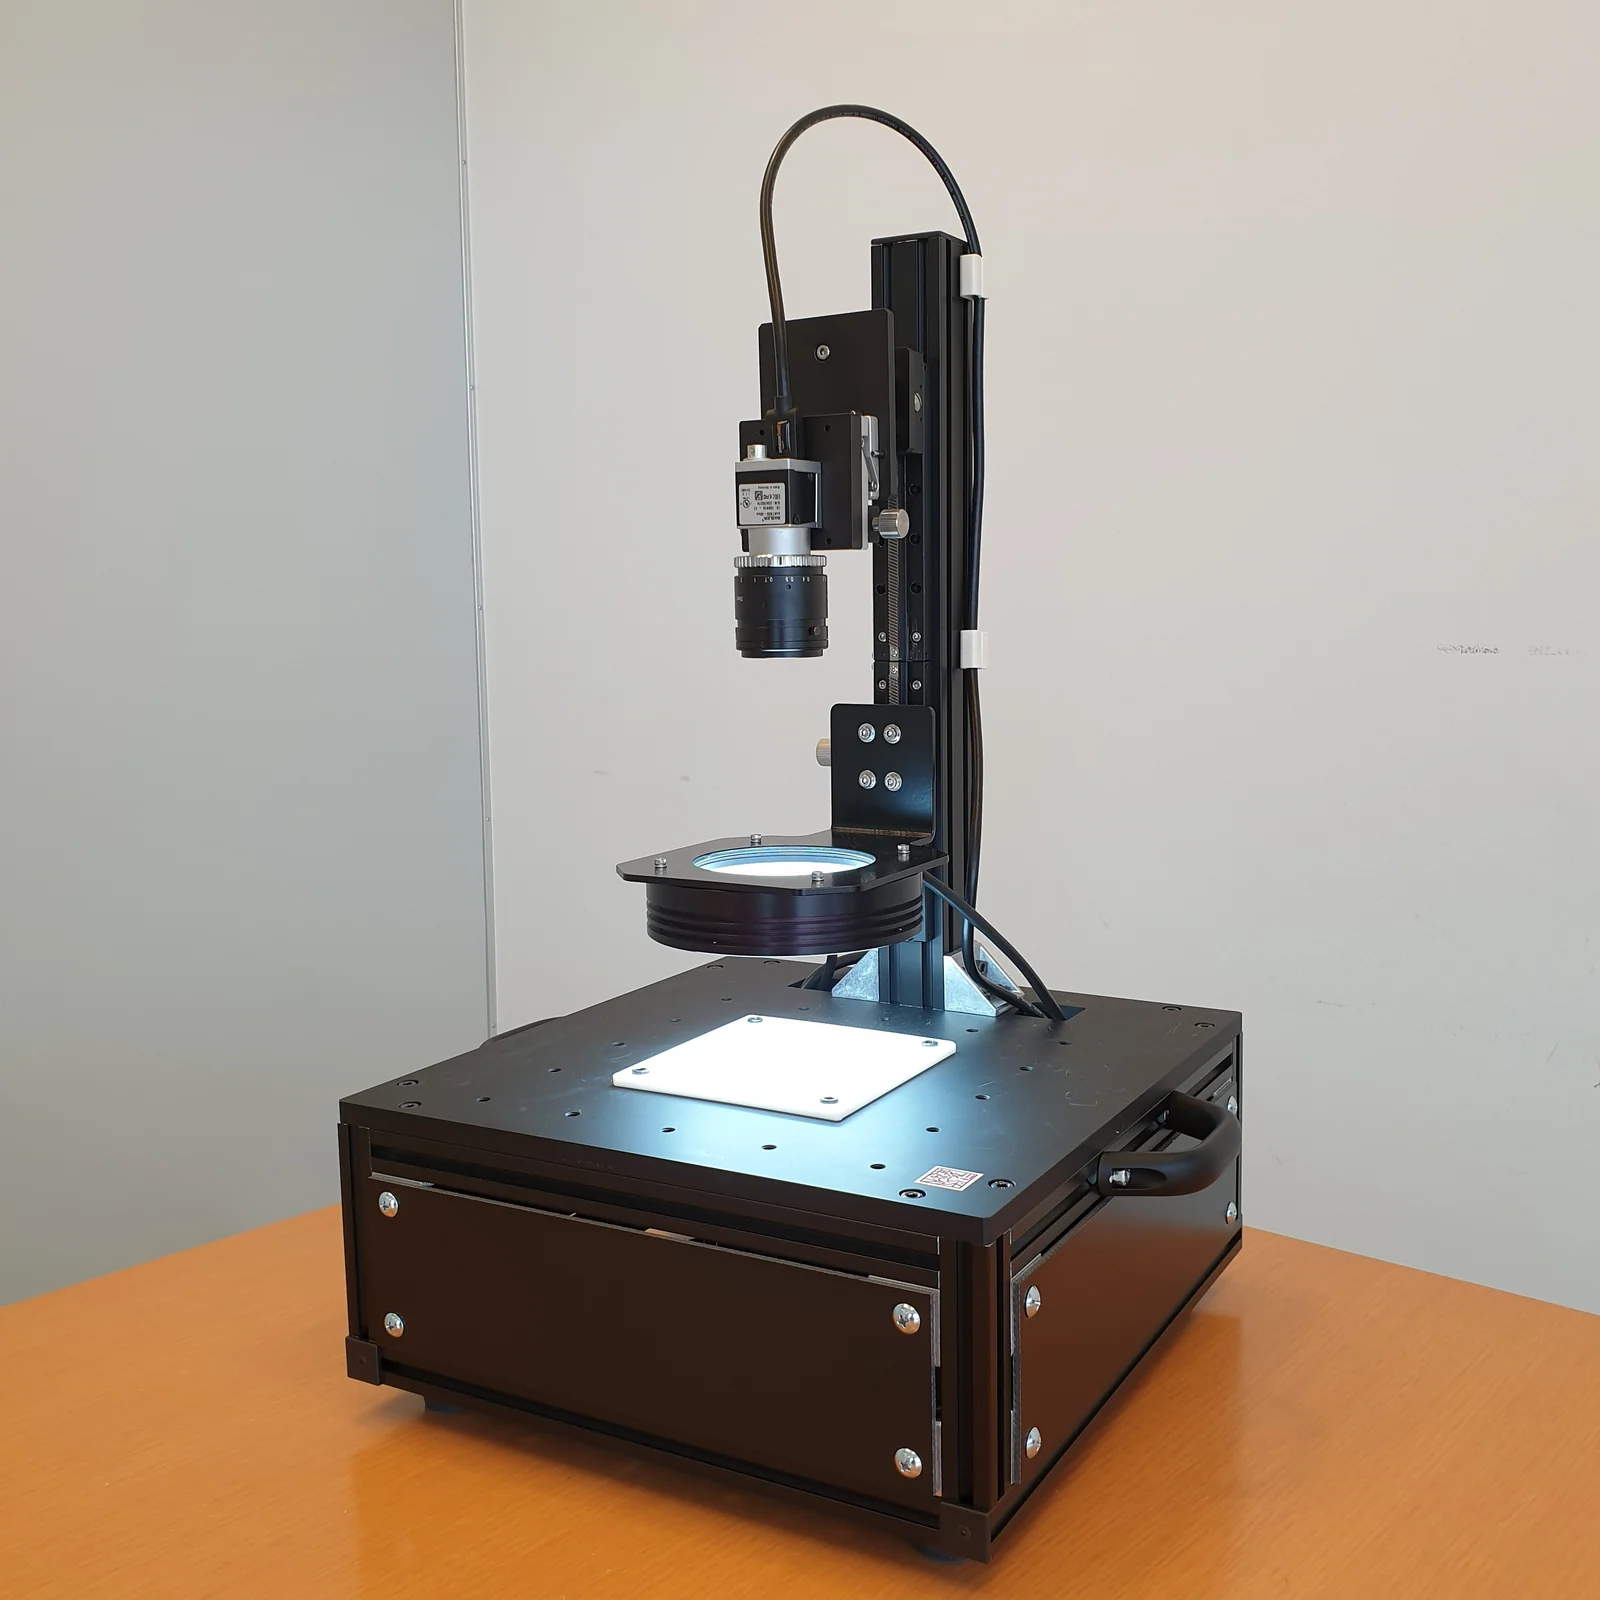
It does not decide; it is devoted to seeing. Place a sample, press the button, and the four outputs come back.
Read more →
Contact
If what you need to see
is not yet visible.
Tell us the material of the object, the size of the defect you need to catch and your current inspection process, and we will work out together whether TR-100 can show it and which configuration fits. A trial capture on your own sample can be arranged.